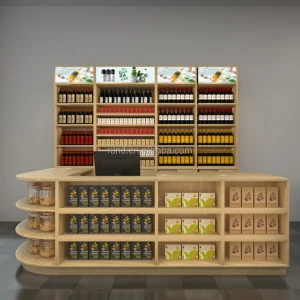
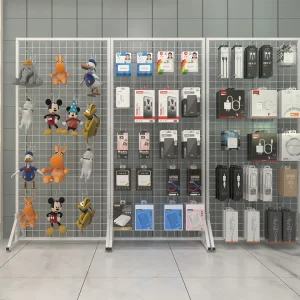
High-performance metal shelving, heavy-duty racking, and automated cashier units engineered to international standards.
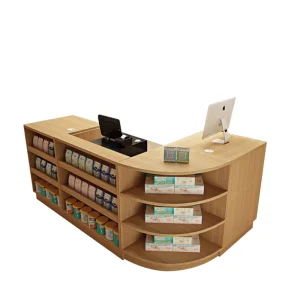
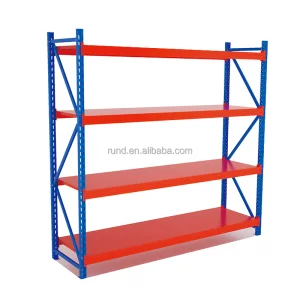
The global retail storage and industrial warehouse equipment industry is undergoing a structural paradigm shift. Driven by the rapid acceleration of omnichannel fulfillment, localized micro-hubs, dynamic store layouts, and automated warehouse infrastructure, global enterprises require storage solutions that deliver high load density, structural longevity, and extreme architectural adaptability.
As supply chain operational expenses continue to rise, international buyers—ranging from multinational supermarket chains and bulk cash-and-carry wholesalers to 3PL logistics networks—are increasingly scrutinizing the Total Cost of Ownership (TCO) of their store fixtures and racking systems. Maximizing vertical footprint density while maintaining safety compliance with rigorous global frameworks (such as AS4084 in Australasia, OSHA/ANSI in North America, and FEM 10.2.02 in Europe) has become an essential competitive imperative.
In this context, securing direct factory partnerships with China’s premier manufacturing clusters—specifically within the Pearl River Delta industrial ecosystem—provides enterprise procurement leaders with an unprecedented balance of economies of scale, metallurgy innovation, and engineering precision. China wholesale retail storage factories are no longer merely low-cost fabricators; they have evolved into advanced technological engineering centers capable of delivering bespoke structural calculations, automated robotic racking, and zero-defect quality control.
Founded in 2016, Dongguan Dingguan Metal Products Co., Ltd. (DirectRack) stands as a premier technology-driven warehouse equipment and commercial retail fixture enterprise headquartered in Dongguan, Guangdong Province—the global epicenter of high-precision metal manufacturing.
Leveraging over 10 years of deep industry expertise combined with an intensive 8-year international export background, DirectRack operates a state-of-the-art manufacturing infrastructure spanning 25,000 square meters of specialized production space. Our sustained annual export revenue consistently exceeds $18 million USD, supplying tier-1 commercial retail racks, heavy-duty industrial pallet systems, and cashier counter units to global logistics hubs and retail chains worldwide.
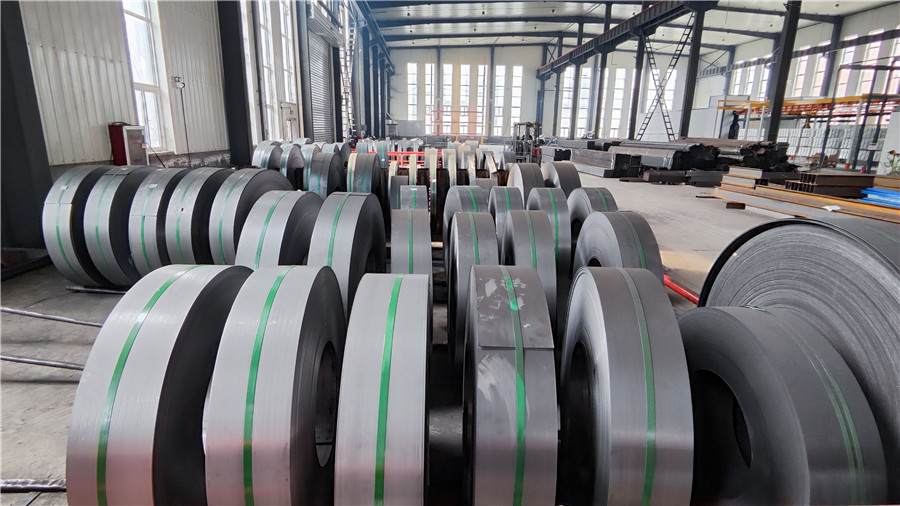
Uncompromising structural integrity defines DirectRack's engineering ethos. Our quality governance is rigorously enforced by a team of 28 specialized QC inspectors who monitor every stage of manufacturing—from raw coil metallurgy validation to final sea-freight packaging.
Our quality control framework strictly adheres to international AS4084 (Steel Storage Racking) and OSHA industrial safety guidelines. Every manufacturing batch undergoes mandatory, standardized quality verification procedures, including:
Utilizing a seamlessly integrated OEM/ODM trade background, DirectRack has established strategic supply chain alliances with over 650 supply chain partners spanning certified raw steel mills, cold-rolling specialists, and automated surface coating plants. Our major international export markets encompass Southeast Asia, the Middle East, and South America, servicing client profiles ranging from high-capacity retail distribution hubs and automotive component facilities to commercial FMCG wholesale operations.
Innovation remains the core catalyst of our operations. Spearheaded by 35 senior R&D engineers, DirectRack utilizes dynamic structural calculation modeling software (FEA) to provide fully bespoke modular storage designs. Our custom engineering capabilities include adjustable shelf depth/height ratios, multi-tier mezzanine configurations, anti-seismic cross-bracing systems, and customized RAL color palettes. Demonstrating our rapid innovation cycle, DirectRack successfully introduced 42 new product designs in the preceding year alone to address the growing demands of automated retail fulfillment.
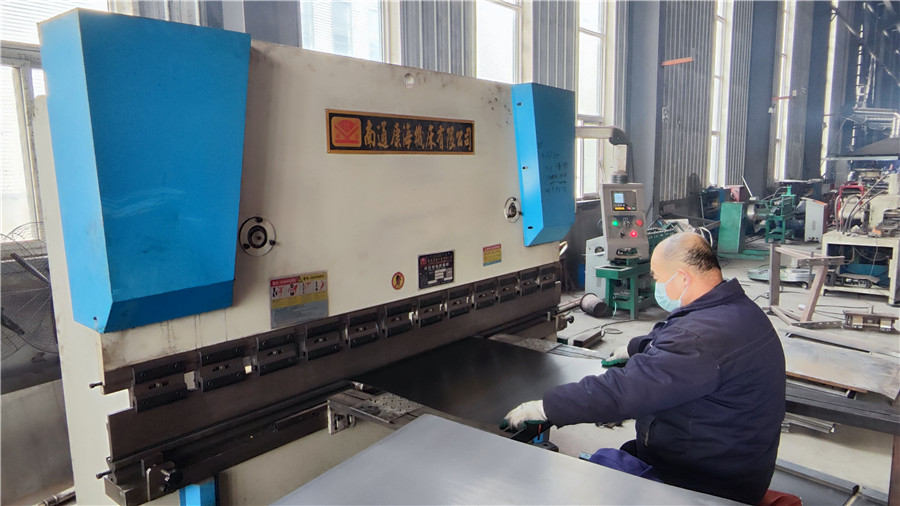
Our 25,000 m² Dongguan facility integrates fully automated production lines designed for maximum material utilization, tight structural tolerances, and batch-to-batch repeatability. Below is a detailed view of our multi-stage production steps and specialized machinery inventory:
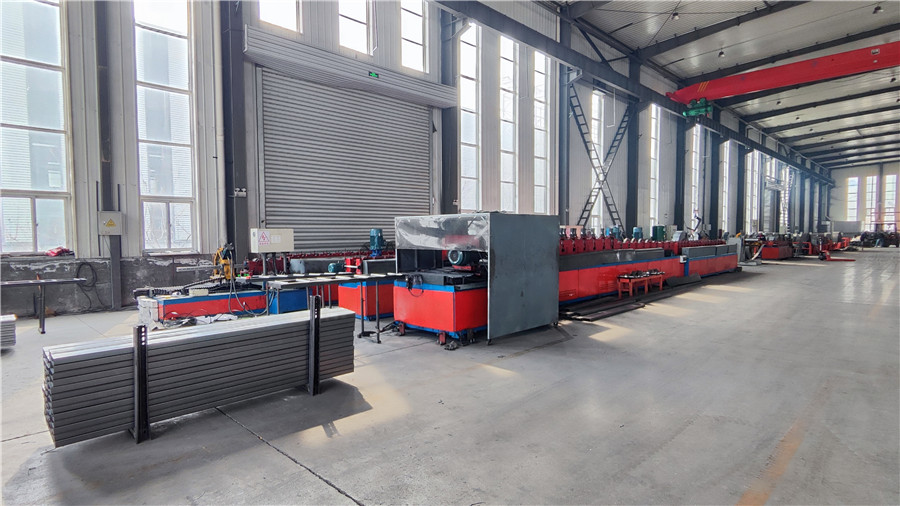
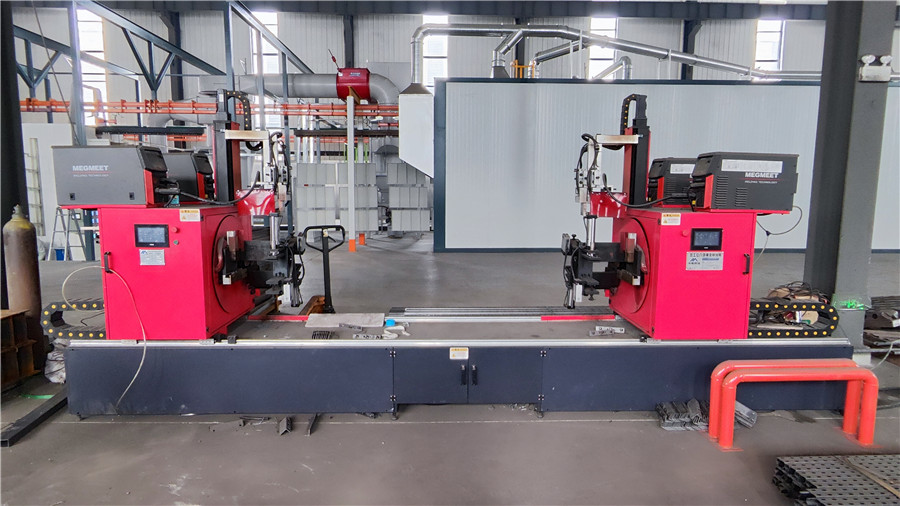
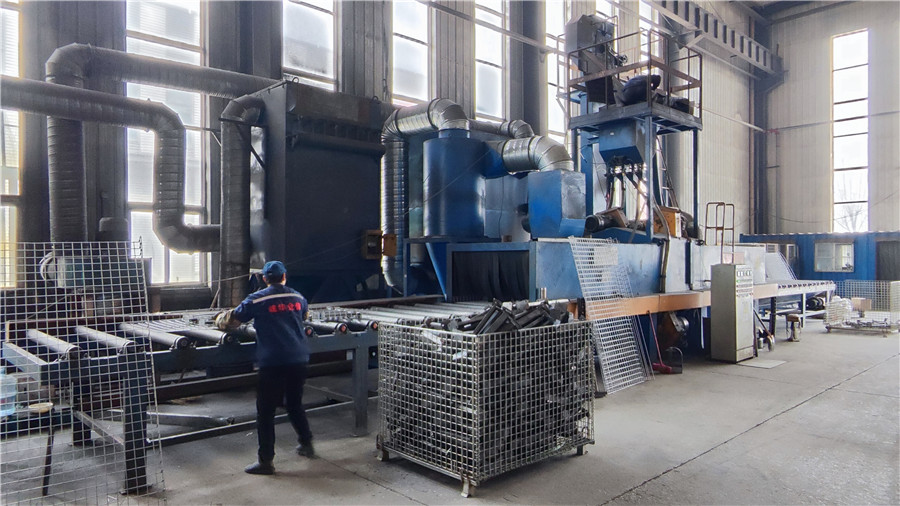
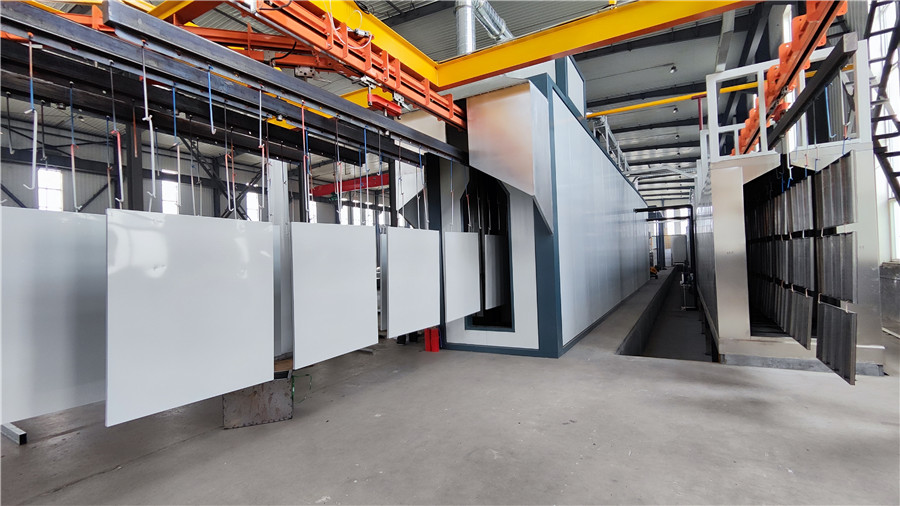
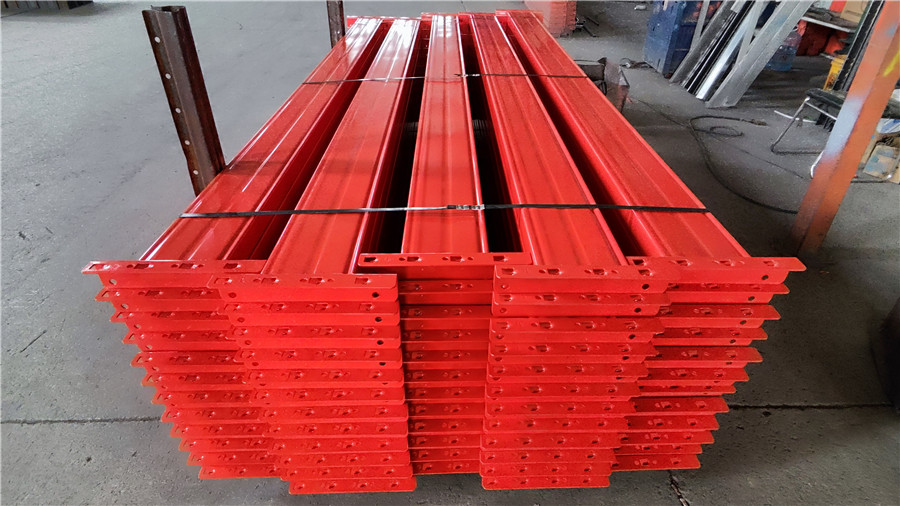
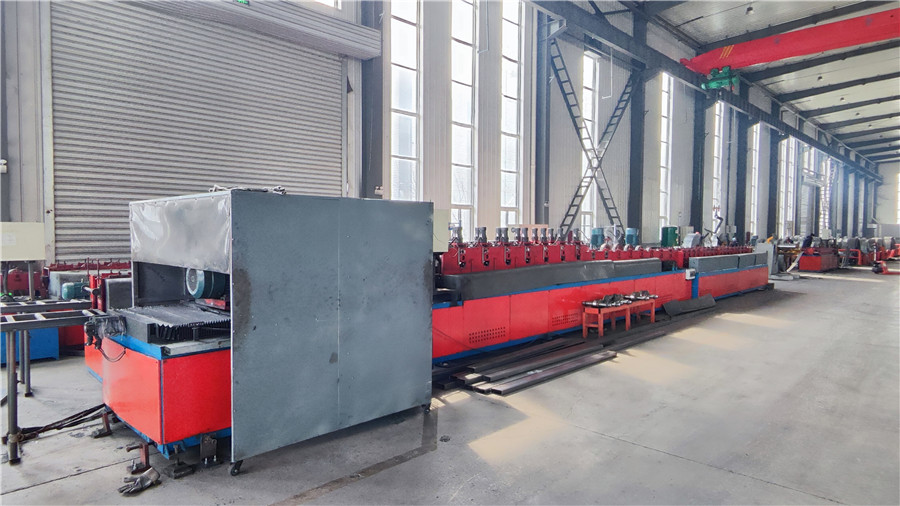
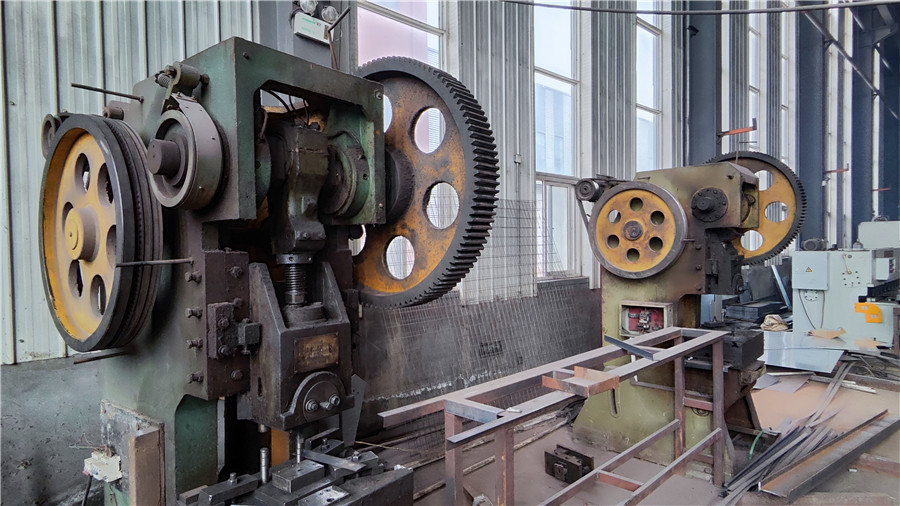
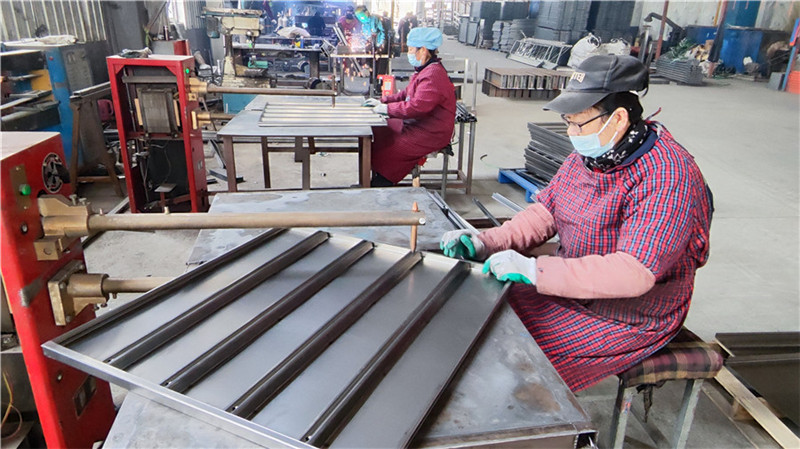
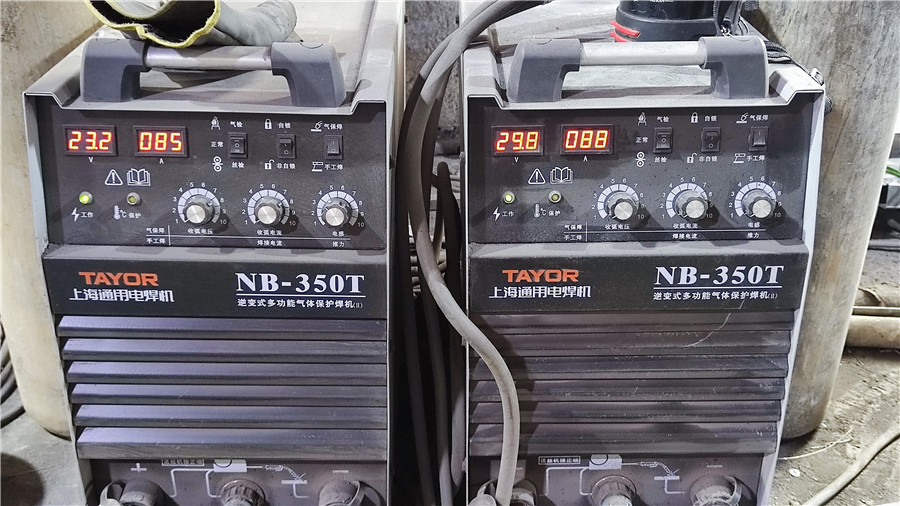
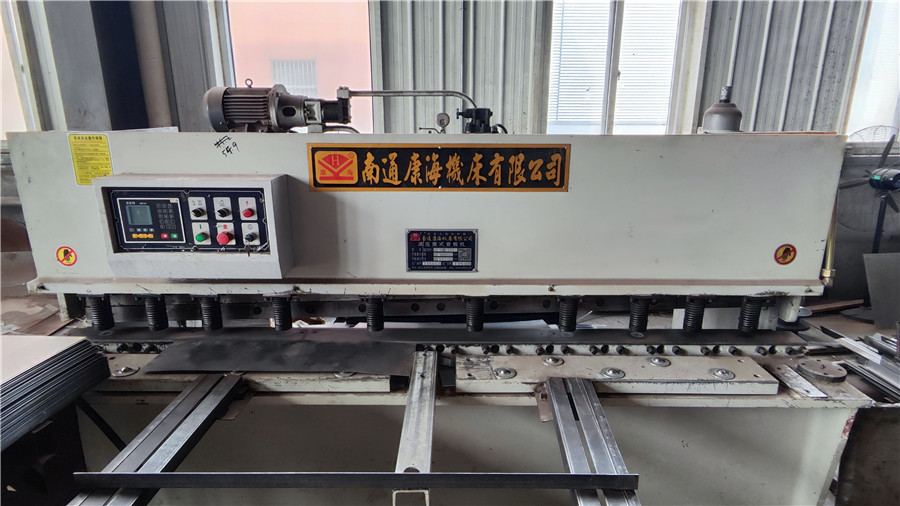
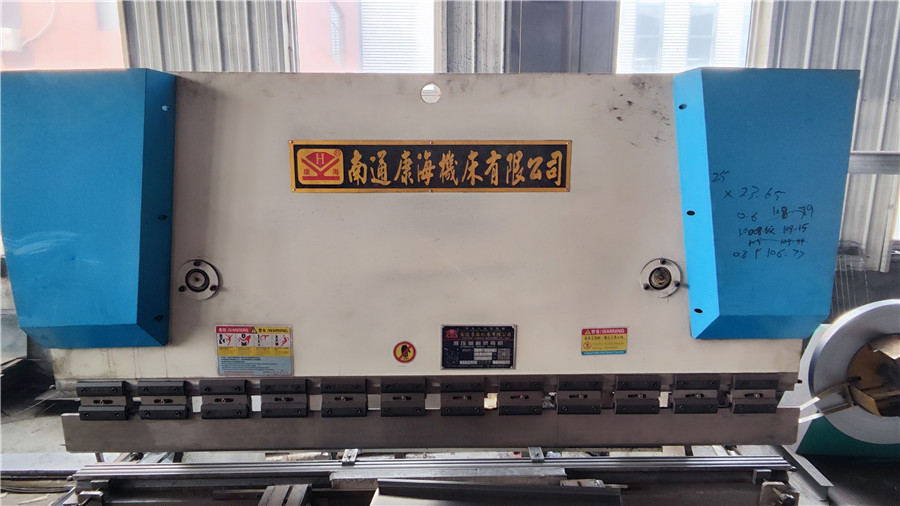
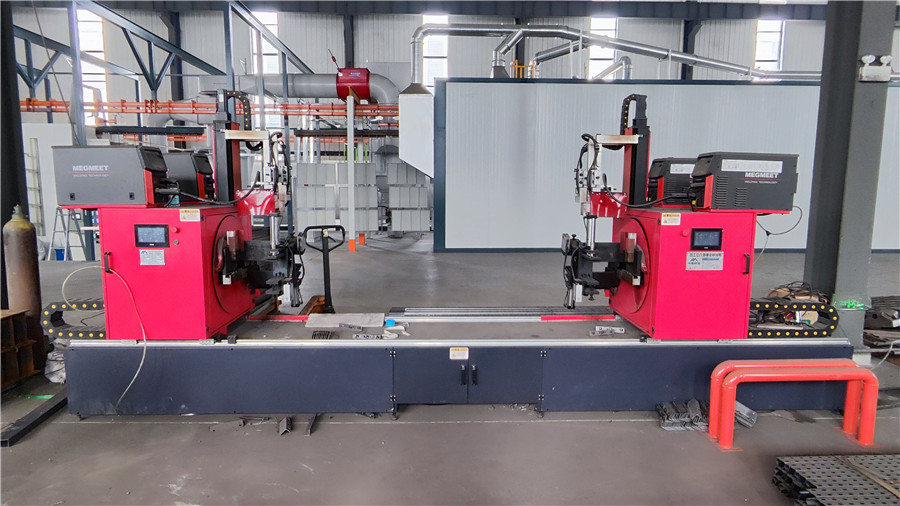
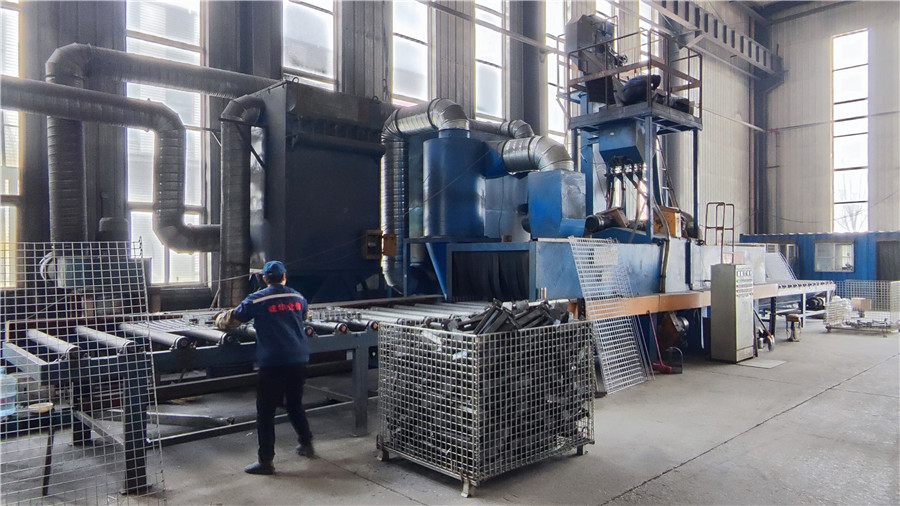
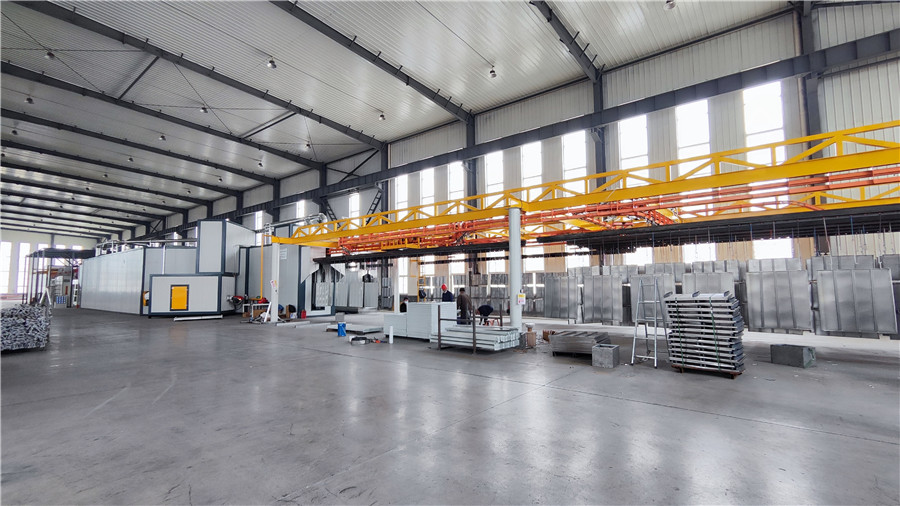
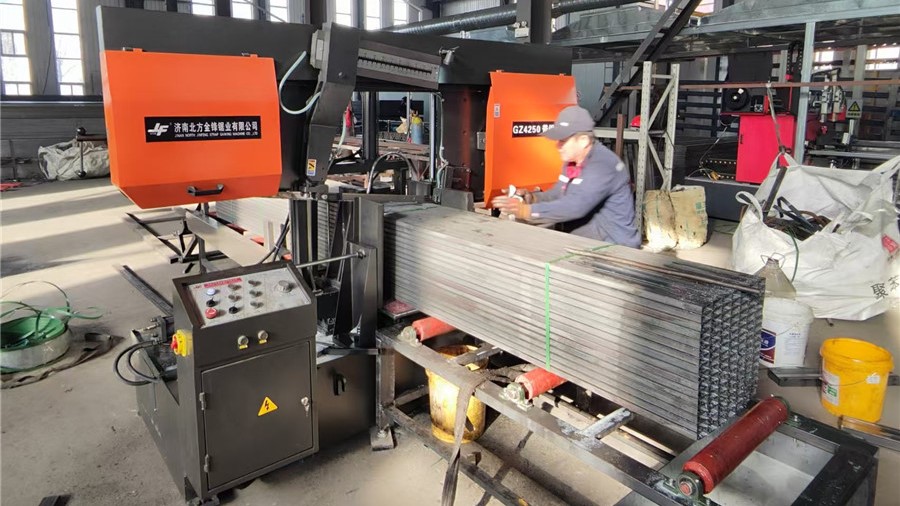
The global storage equipment procurement sector is heavily influenced by steel raw material sourcing, automated processing speeds, and supply chain synergy. Sourcing direct from China wholesale retail storage factories such as DirectRack provides significant operational efficiencies over traditional Western suppliers:
| Evaluation Vector | Direct Factory DirectRack (Dongguan, China) | Traditional Regional Distributors |
|---|---|---|
| Raw Material Purchasing | Direct bulk mill integration (Baosteel/Shougang Q235B & Q355B high-tensile steel) | Secondary distributor markups; constrained batch volume access |
| Manufacturing Automation | Robotic mesh welding, continuous cold-roll forming, automated powder lines | Semi-automated or manual labor intensive fabrication |
| Customization Engineering | In-house R&D (35 Engineers); FEA simulation & bespoke mold creation | Limited to standard off-the-shelf structural dimensions |
| Lead Times & Capacity | 25,000 m² facility; 100+ high-capacity container shipments per month | Dependence on third-party replenishment cycles |
| Cost Optimization | Direct OEM/ODM pricing yielding 25%–45% procurement cost reduction | Layered broker margins and inflated warehousing overheads |
Furthermore, Dongguan’s proximity to Shenzhen and Guangzhou port infrastructure optimizes container dispatch efficiency, ensuring fast freight turnaround to North America, Europe, Southeast Asia, and the Middle East.
Modern retail and warehouse environments demand specialized storage typologies aligned with specific product velocity, load profiles, and customer presentation standards. DirectRack manufactures solutions optimized across multiple enterprise domains:
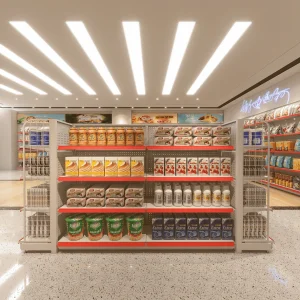
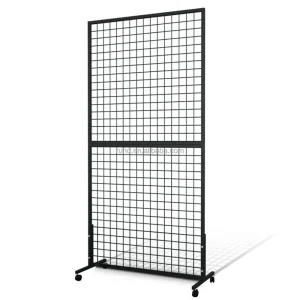
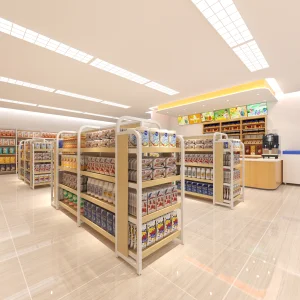
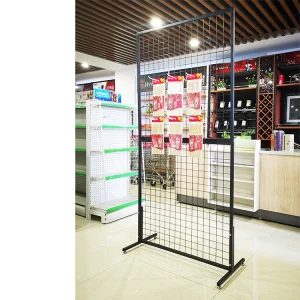
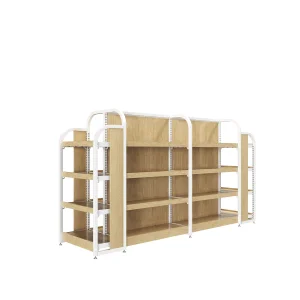
Utilizing single and double-sided heavy-duty gondola units equipped with solid steel wall panels or wire grid backings. Integrated wooden accents and promotion tables enhance visual merchandising while supporting load capacities up to 150 kg per shelf layer.
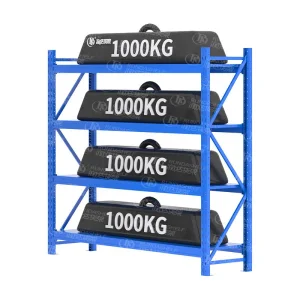
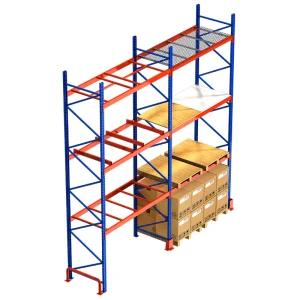
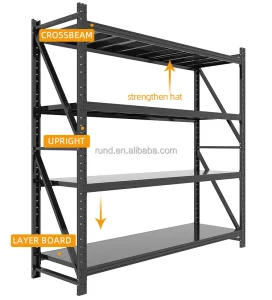
Multi-level adjustable heavy-duty rack systems designed for European standard pallets. Configured with teardrop or beam locking mechanisms, these systems integrate seamlessly with Automated Guided Vehicles (AGVs) and warehouse robotics for dense horizontal and vertical space utilization.
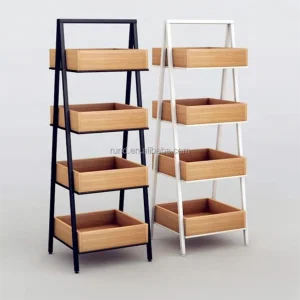
Combining aesthetic steel-and-wood hybrid shelving systems to present a warm, high-end consumer ambiance without compromising structural rigidity. Fully adjustable shelf pitch angles allow optimized visibility for small SKUs.
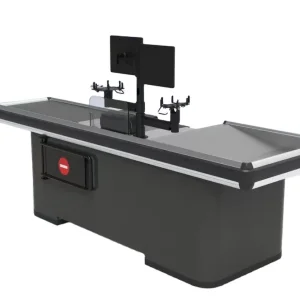
High-durability checkout counters constructed with MDF wood, stone-look composite countertops, and anti-impact corner protection. Equipped with integrated wire routing channels and scanner mount brackets for seamless POS operation.
As smart warehousing and automated retail continue to evolve, the physical infrastructure of retail storage must adapt. DirectRack’s R&D roadmap tracks four critical industry trends:
Address key technical, structural, and commercial inquiries regarding factory sourcing and procurement from DirectRack.
Discover additional boltless shelves, display panels, checkout systems, and retail accessories from our factory.
 DirectRack