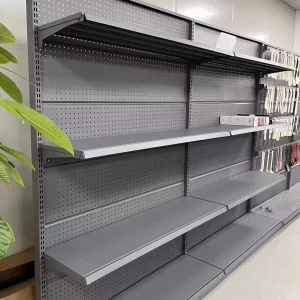
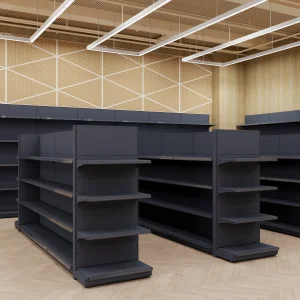
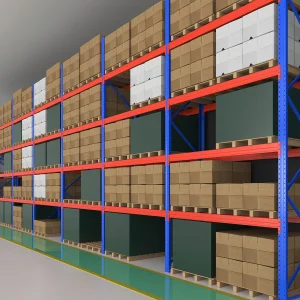
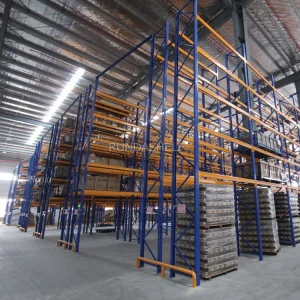
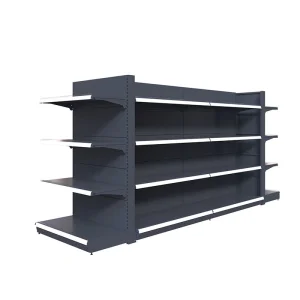
Explore our foundational range of heavy-duty storage racks and modular retail display systems designed for high scalability.
An in-depth analysis of supply chain modernization, structural optimization, and dynamic industrial shelving systems.
As logistics operations pivot towards complete automation, traditional racking systems must evolve. Warehouses now require high-precision fabrication tolerances. Standard rack structures are no longer compatible with modern Automatic Storage and Retrieval Systems (AS/RS). Dynamic shuttle systems, Automated Guided Vehicles (AGVs), and automated stacker cranes demand straightness tolerances exceeding standard regulatory Baselines. Custom OEM factories must utilize advanced cold-forming lines to achieve structural deviations below +/- 1mm over the entire frame height.
Global logistics hubs are increasingly built in regions subject to high seismic activity. High-density racking structures act as heavy inverted pendulums under earthquake loads. Modern engineering demands Finite Element Analysis (FEA) and dynamic stress simulations to optimize column and beam designs. Customized baseplates, heavy-duty floor anchors, and strategically placed cross-bracing configurations absorb kinetic energy. This ensures standard structural stability, compliance with AS4084 and OSHA guidelines, and prevents devastating rack collapses.
Green warehousing is transforming raw material sourcing and manufacturing. Suppliers must adopt non-toxic, eco-friendly surface treatment technologies. Lead-free epoxy powder coatings are the modern industry benchmark, ensuring zero VOC emission lines. Furthermore, custom OEM suppliers are integrating high-durability hot-dip galvanization processes. This method is critical for cold storage, sub-zero food logistics, and chemical processing facilities, protecting steel substrates from accelerated oxidation without structural degradation.
Founded in 2016, Dongguan Dingguan Metal Products Co., Ltd. (DirectRack) represents the peak of custom OEM manufacturing for industrial warehouse storage and high-load retail racking. Operating from our state-of-the-art 25,000 square meter facility in Guangdong, we leverage over 10 years of structural engineering expertise and 8 years of global export compliance to supply premier retail and logistics hubs.
Explore the end-to-end manufacturing process flow of DirectRack, from structural raw steel to custom coated components.
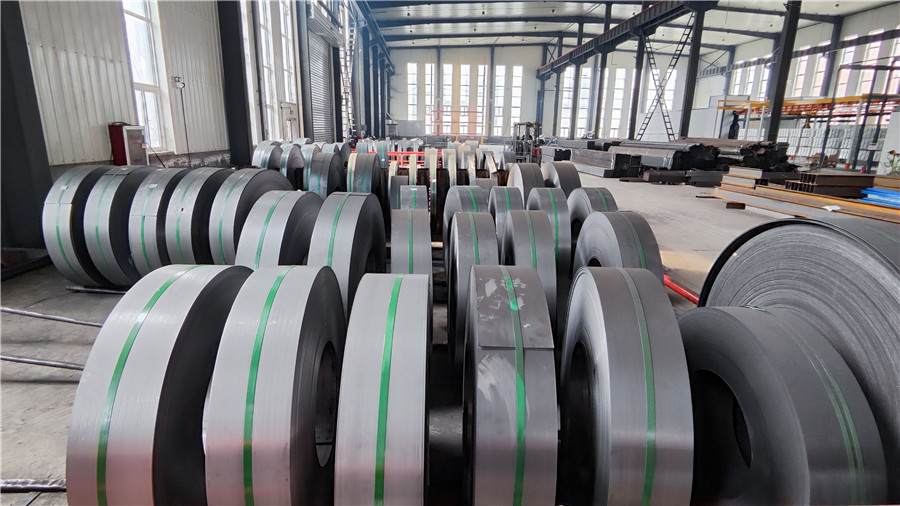
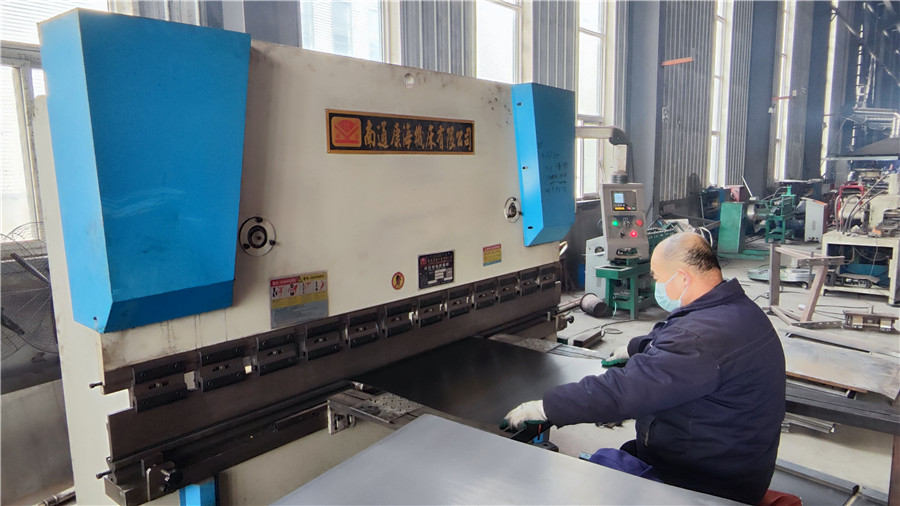
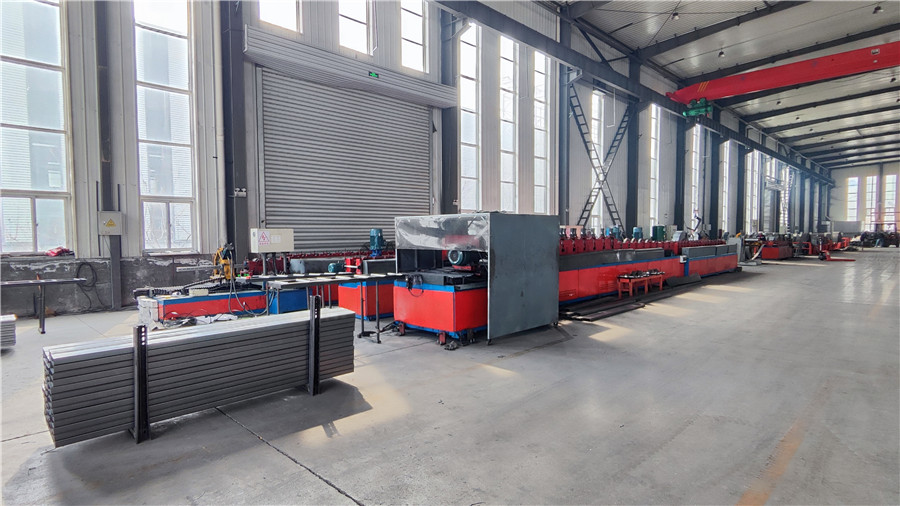
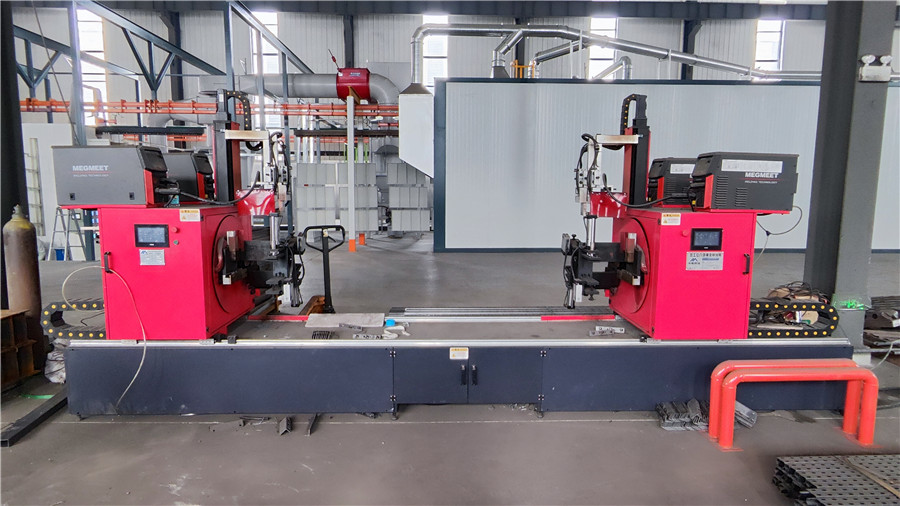
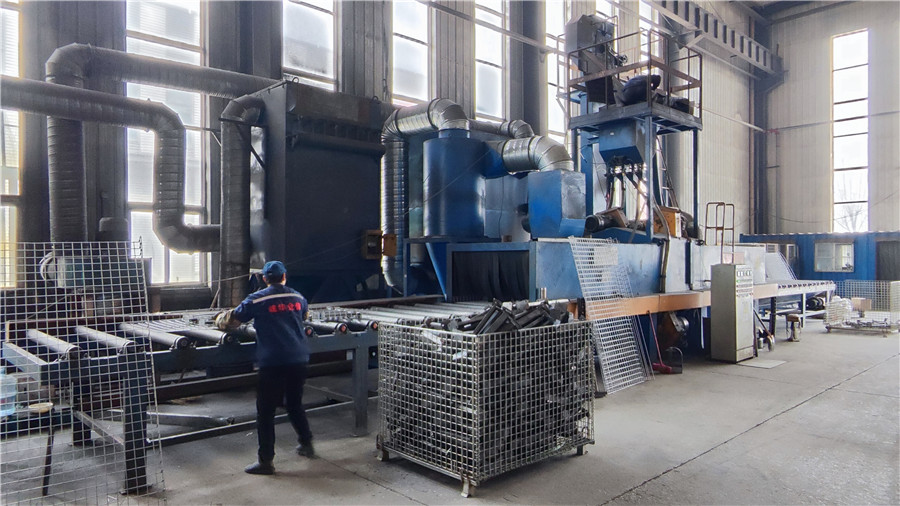
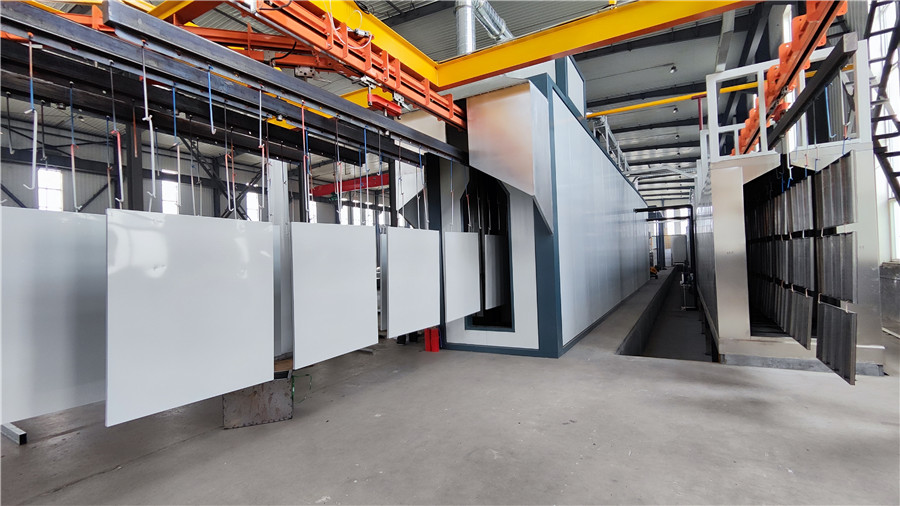
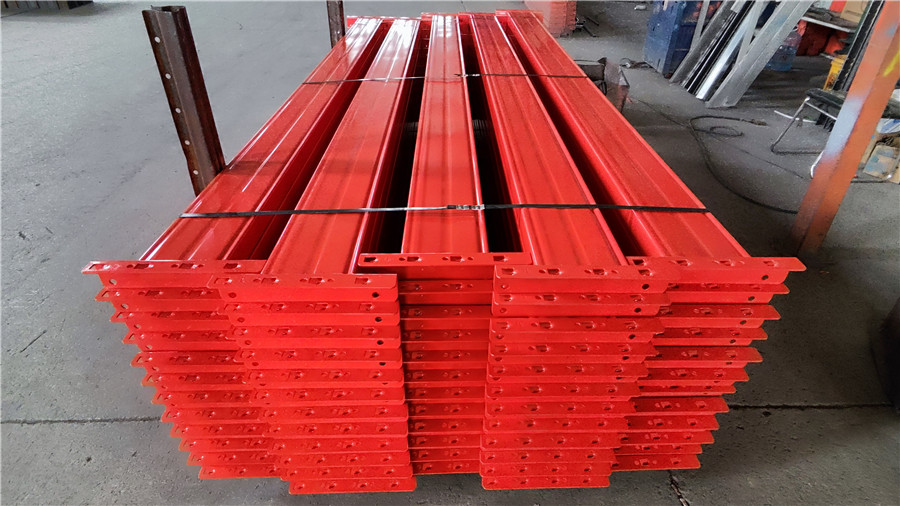
Our facility houses industry-grade fabrication equipment ensuring flawless tolerances and automated quality outputs.
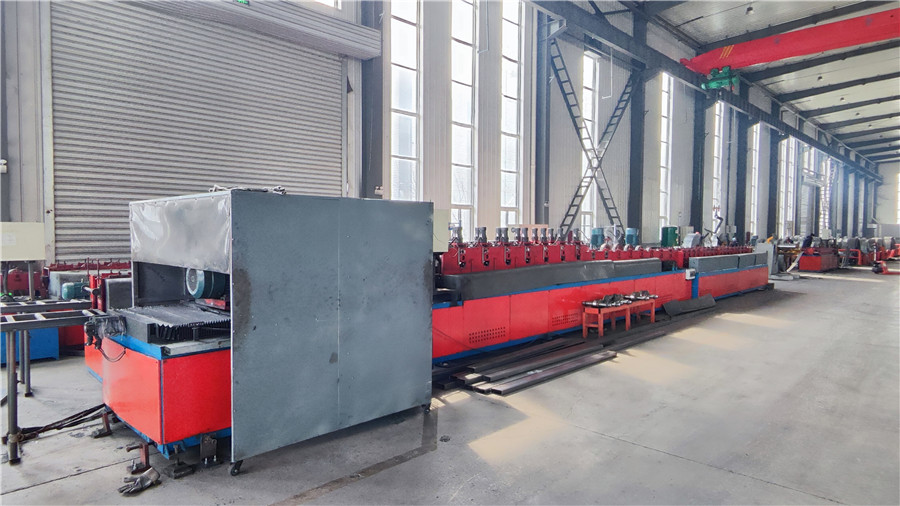
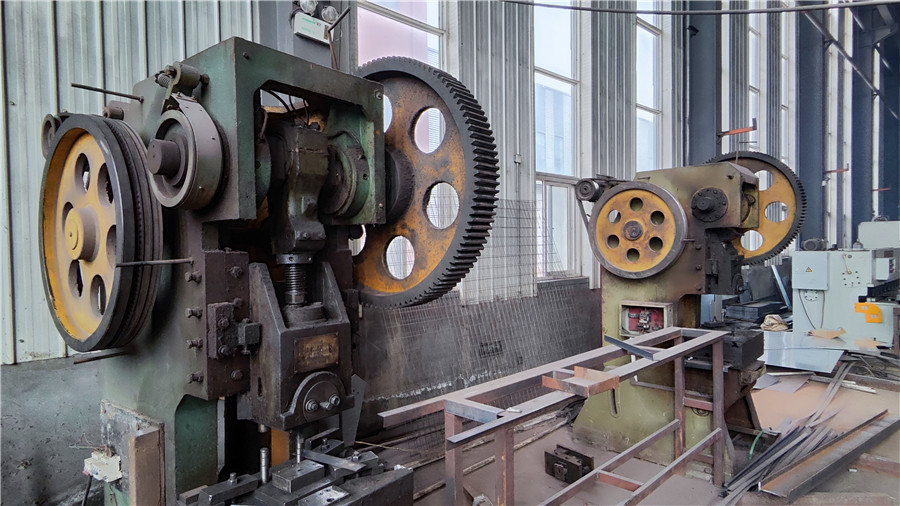
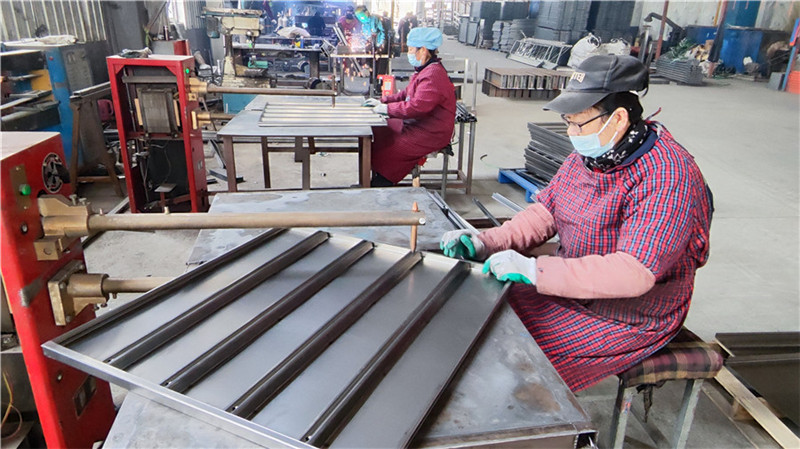
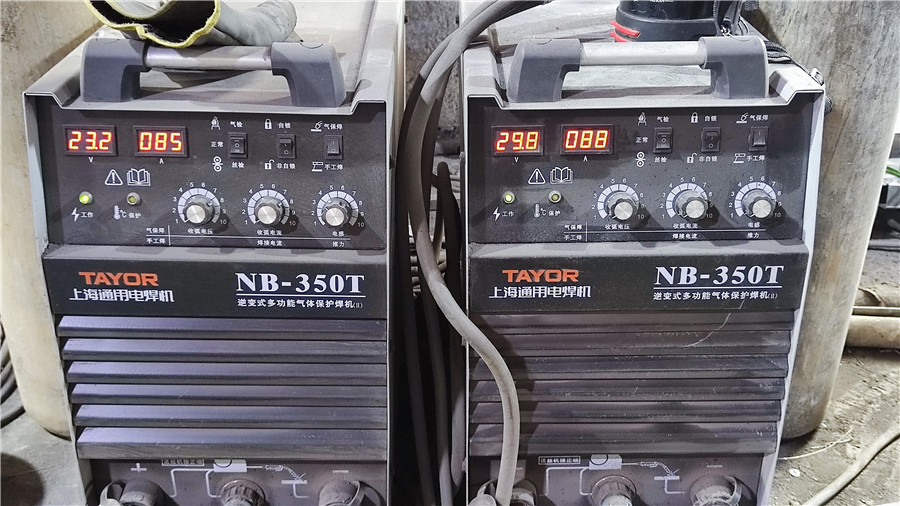
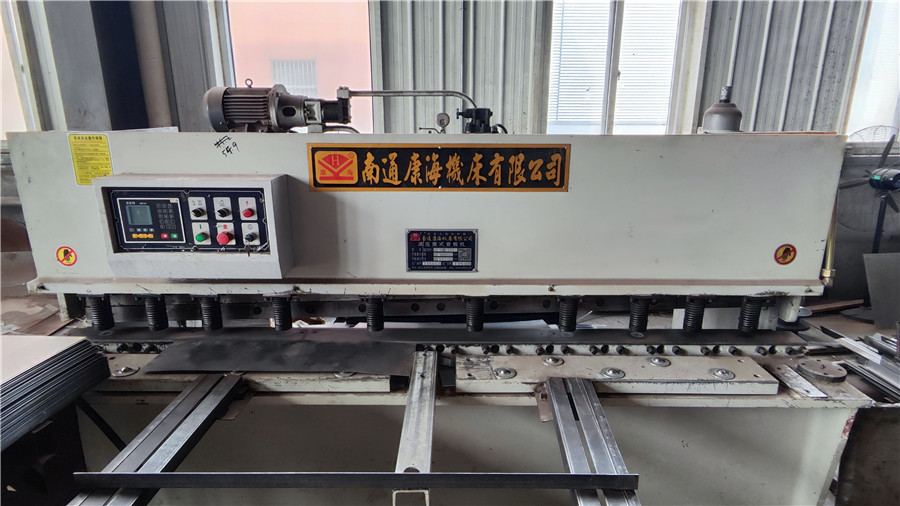
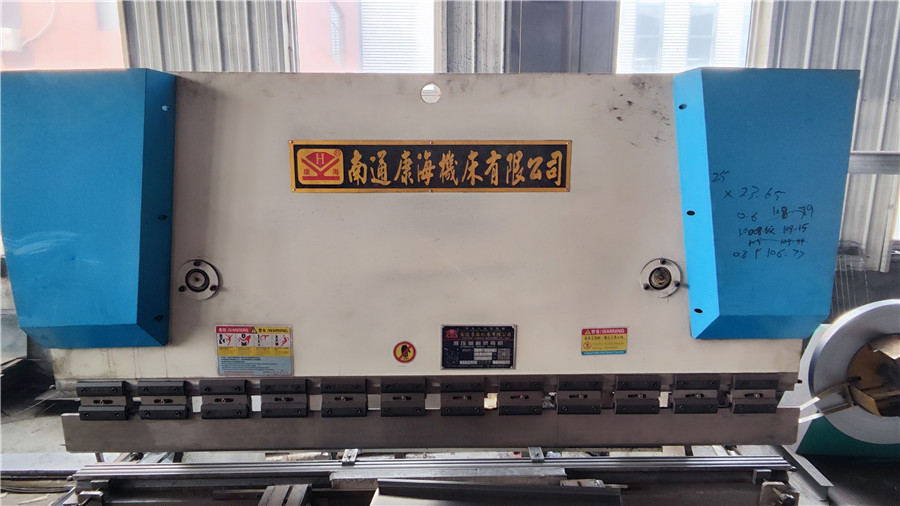
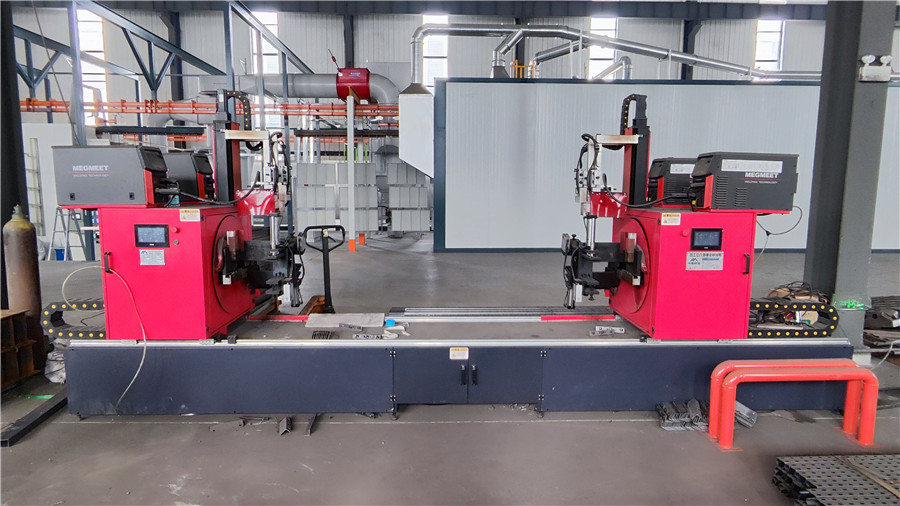
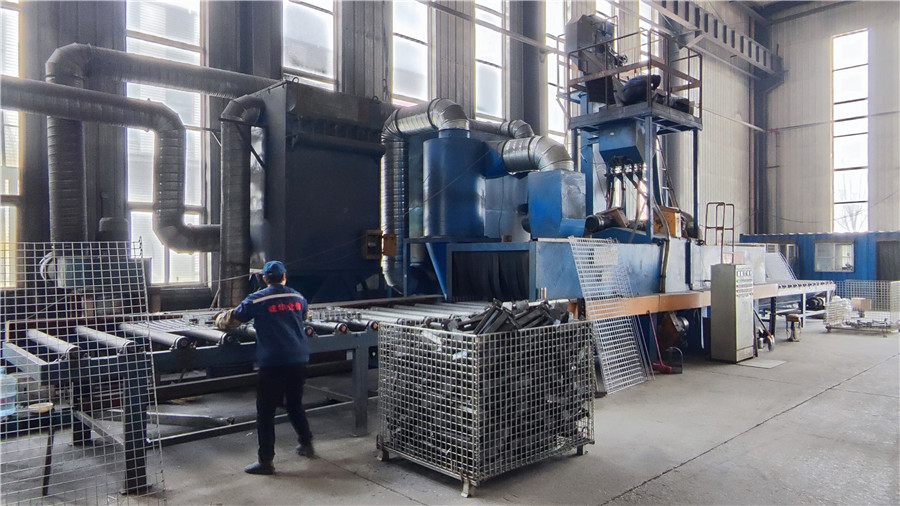
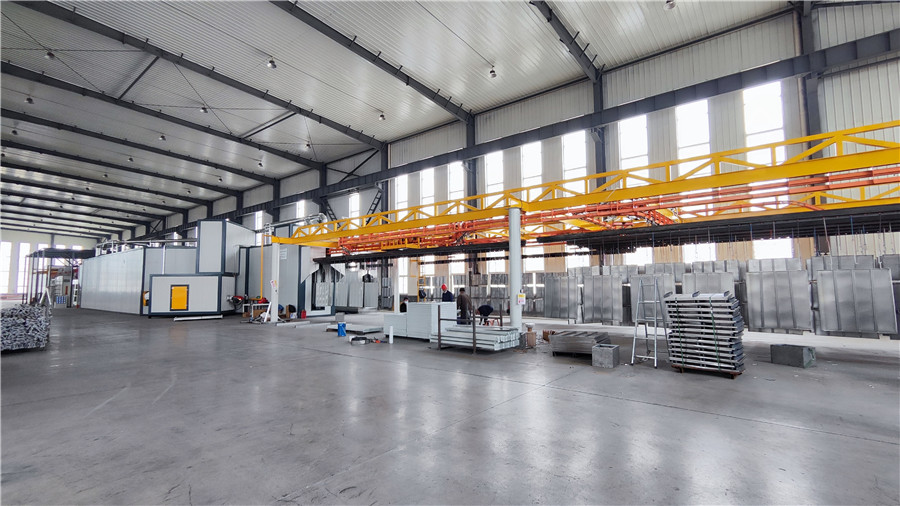
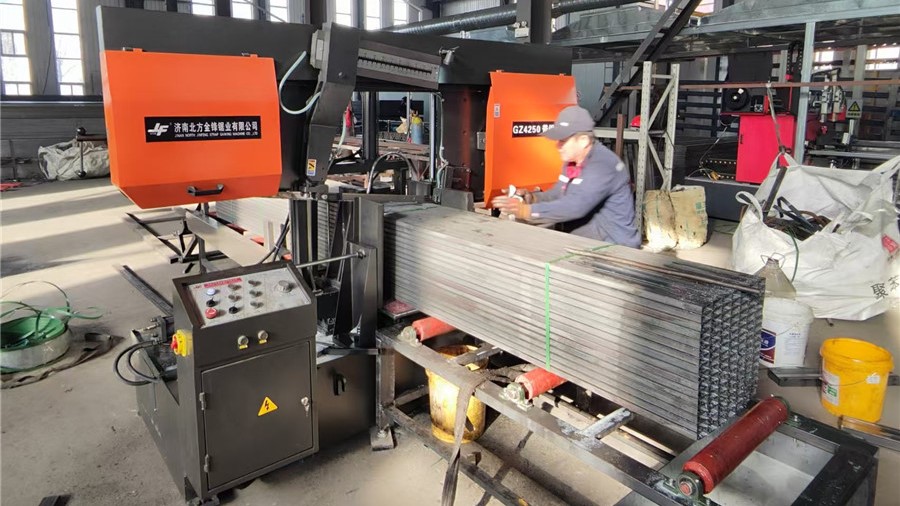
Rigorous mechanical validation protocols to secure ultimate compliance with global industrial safety criteria.
Critical structural connections are continuously examined by 28 qualified QA inspectors utilizing industrial X-ray imaging. This prevents internal gas pocketing, micro-cracks, and welding incomplete fusion zones that could cause structural beam failures under maximum loads.
To resist corrosive wear in industrial settings, protective finishes must exceed a 60-micron thickness. Magnetic digital gauges verify coating uniformity across all shelf and frame batches, ensuring durable protection in high-moisture facilities.
Full-scale vertical compression testing ensures column profiles support maximum loading ratings without buckling. We apply standardized load cell configurations to test beam deflection ratios, guaranteeing safe, high-density storage operations.
Simplifying complex international logistics with optimized container space utilization and localized structural compliance.
By integrating 650 raw material supply partners, DirectRack stabilizes material costs even during high global steel price volatility. We use Q235B and Q355B high-strength structural carbon steel to ensure stable supply chains and competitive lead times.
Exporting to Southeast Asia, the Middle East, and South America requires strict compliance with international standards. Our engineering team customizes all racking calculations to meet AS4084 (Australian Racking Standards) and OSHA guidelines, minimizing import customs delays.
Ocean freight optimization is critical to international procurement. We design smart knockdown racking frames and nesting shelves to maximize ocean container space, reducing shipping costs per unit by up to 35%.
Aligning product development with next-generation smart warehouses and zero-carbon industrial goals.
Developing micro-sensor arrays integrated directly into heavy-duty racking load beams. Real-time stress and deformation data are transmitted wirelessly, alerting operations managers to overloading conditions before failure occurs.
Perfecting continuous forming lines to output single-piece, vertical storage uprights exceeding 24 meters in height. These structural columns feature the precise tolerance ratios required for automated crane tracking systems.
Deploying advanced thermo-curing powder lines that lower energy consumption by 20%. This eco-friendly process improves corrosion resistance, keeping industrial shelves rust-free in damp environments.
Technical guidance on customized configurations, material specifications, and regulatory compliance.
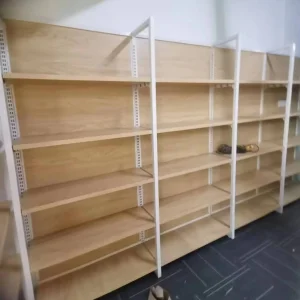
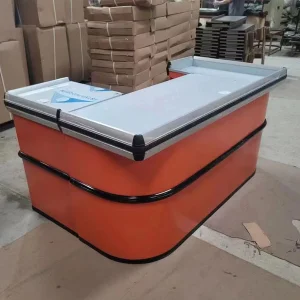
Complete your operations setup with high-capacity gondolas, pallet systems, and specialized retail cash counters.
 DirectRack