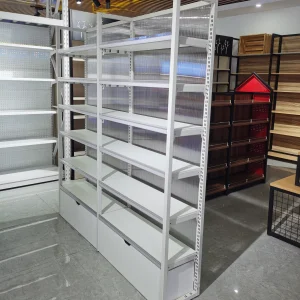
Explore high-performance modular gondolas, wire display racks, and storage platforms engineered for maximum load distribution and optimal visual merchandising.
Analyzing the macro-economic shifts, omni-channel retail transformations, and steel infrastructure evolution shaping commercial shelving procurement worldwide.
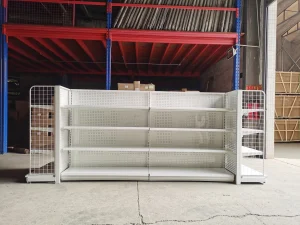
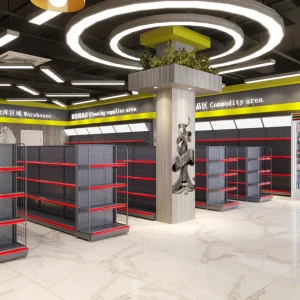
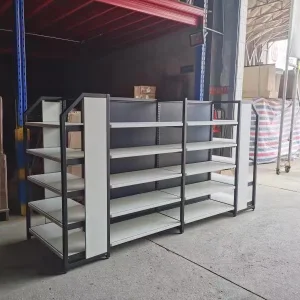
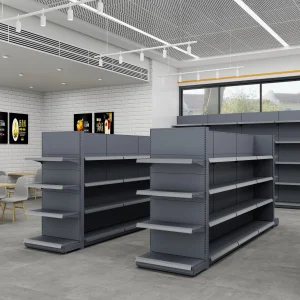
Modern retail environments demand shelving systems that facilitate rapid micro-fulfillment alongside traditional customer browsing. Gondola systems are evolving into modular hubs equipped with integrated wire pathways, click-and-collect holding zones, and high-density loading thresholds capable of handling high stock turnover.
Transitioning from basic mild steel to high-yield Q235B and Q355B cold-rolled steel profiles ensures higher weight capacities with thinner, sleeker structural footprints. Modern multi-stage zinc phosphate pre-treatments and electrostatic powder coatings dramatically increase corrosion and scratch resistance in high-traffic commercial spaces.
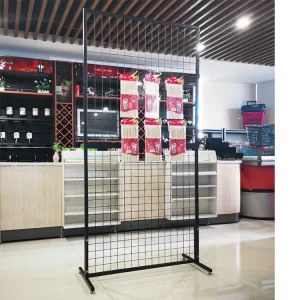
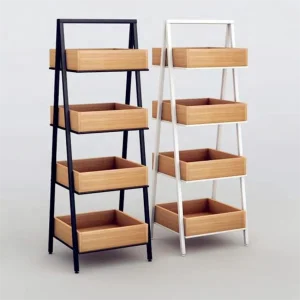
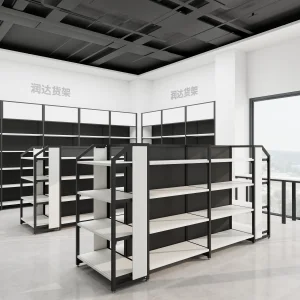
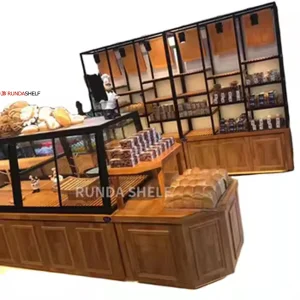
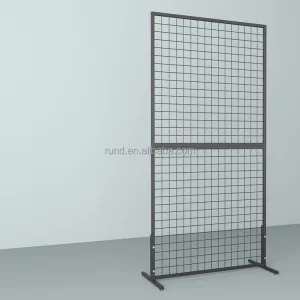
Top global exporters are shifting toward hybrid steel-wood island configurations. Boutiques, convenience chains (e.g., KKV, Miniso styles), and hypermarkets require modular back panels—ranging from pegboards and gridwalls to flat metallic and acoustic timber panels—enabling visual reconfiguration in minutes without specialized tooling.
Global supply chain surveys indicate that top-tier retail chains evaluate suppliers not merely on FOB unit price, but on Total Cost of Ownership (TCO), knock-down volume efficiency during ocean freight, and strict structural compliance under AS4084 and OSHA standard loading protocols.
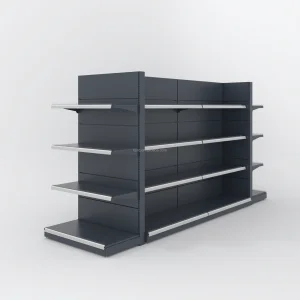
Understanding the stress distribution, vertical column profiles, cantilever bracket bending moments, and structural deflection thresholds across industrial gondola systems.
| Structural Parameter | Standard Commercial Gondola | Heavy-Duty Supermarket Gondola | Industrial Warehouse Integrated |
|---|---|---|---|
| Primary Material Grade | Q195 Cold-Rolled Steel | Q235B High-Tensile Steel | Q355B Structural Alloy Steel |
| Upright Column Profile | 30 x 60 x 1.5mm Pitch 25mm | 30 x 80 x 2.0mm Pitch 50mm | 50 x 100 x 2.5mm Heavy Pitch |
| Shelf Panel Thickness | 0.5mm – 0.6mm Reinforced | 0.7mm – 0.8mm Dual Stiffener | 1.0mm – 1.2mm Box Ribbed Design |
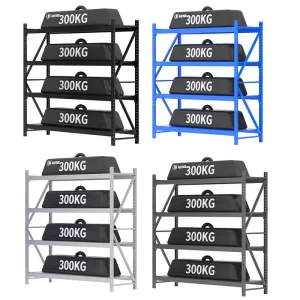
| Max Distributed Load / Tier | 45 kg – 65 kg | 100 kg – 180 kg | 300 kg – 1000+ kg Beam Support |
| Surface Finish Spec | 40-60µm Electrostatic Powder | 60-80µm Thermoset Epoxy Powder | 80-100µm Anti-Scratch Outdoor/Industrial |
| Safety Deflection Standard | L / 200 Max Deflection | L / 250 ISO Compliant | AS4084 Structural Rigidity Deflection |
Leading the market in precision manufacturing, automated roll-forming, global compliance, and end-to-end OEM/ODM customized commercial display solutions.
Founded in 2016, Dongguan Dingguan Metal Products Co., Ltd. (DirectRack) is a technology-driven warehouse equipment enterprise located in Dongguan, Guangdong Province. Leveraging 10 years of industry expertise and 8 years of international export background, the company operates a state-of-the-art manufacturing plant covering 25,000 square meters of building area. Our annual export revenue consistently exceeds $18 million USD, supplying premium steel storage systems to worldwide logistics networks.
DirectRack maintains strict quality governance enforced by 28 specialized QC inspectors. Our quality control framework adheres to international AS4084 and OSHA safety standards. Our standard product inspection methods include X-ray weld seam analysis, coating thickness measurement via magnetic gauge, column compression destruction tests, and full-scale beam deflection loading tests to ensure zero-defect delivery.
Utilizing a seamlessly integrated OEM/ODM trade background, DirectRack has established strategic alliances with 650 supply chain partners across raw steel sourcing and automated surface treatment industries. Our primary export markets include Southeast Asia, the Middle East, and South America. Our main client types range from retail distribution facilities and automotive parts warehouses to commercial FMCG wholesale hubs.
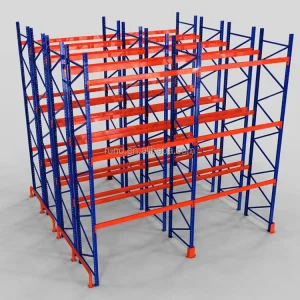
Innovation is at the core of our business model. Spearheaded by 35 senior R&D engineers, DirectRack provides dynamic structural calculation models and fully bespoke modular storage designs. Our custom options feature customizable shelf depth/height ratios, multi-tier mezzanine configurations, anti-seismic bracing, and custom RAL color palettes. In the previous year, we successfully introduced 42 new product designs to meet evolving automated warehouse demands.
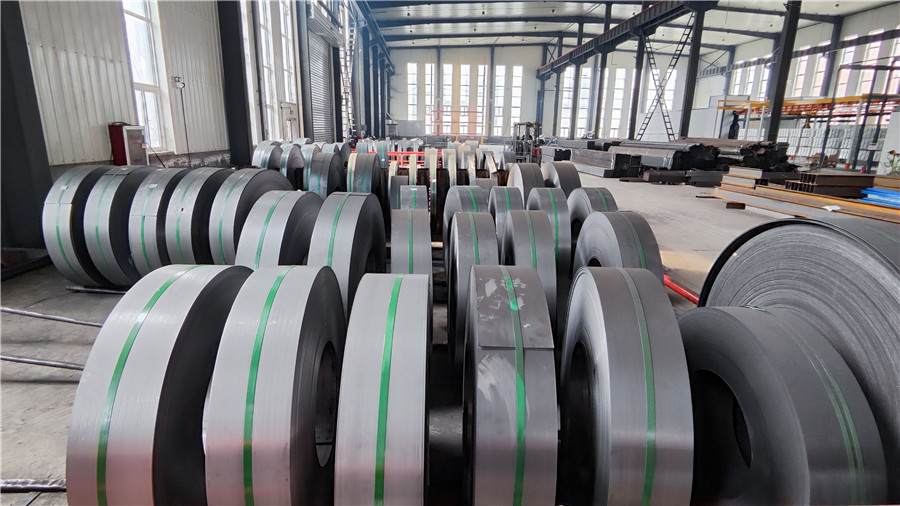
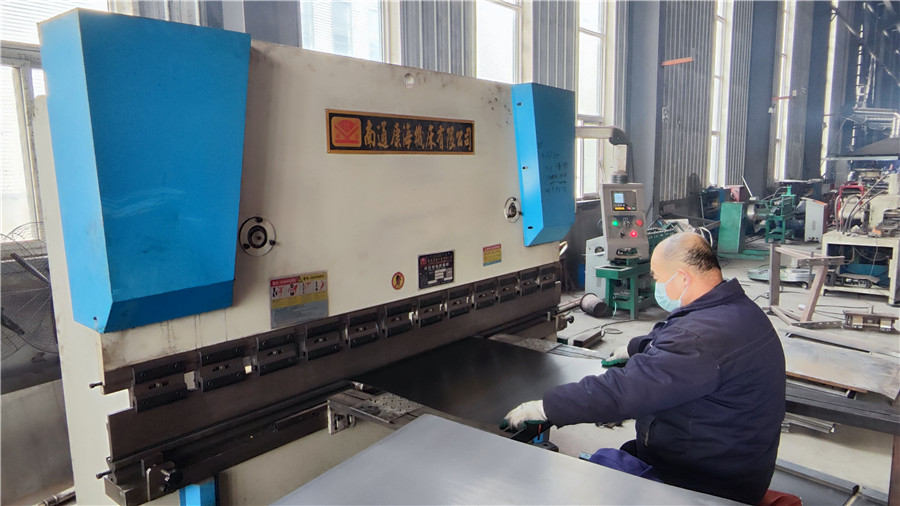
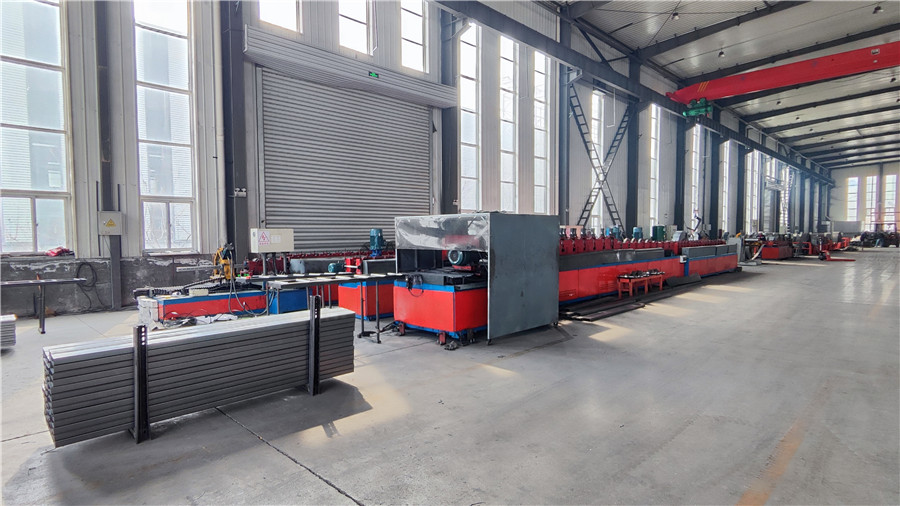
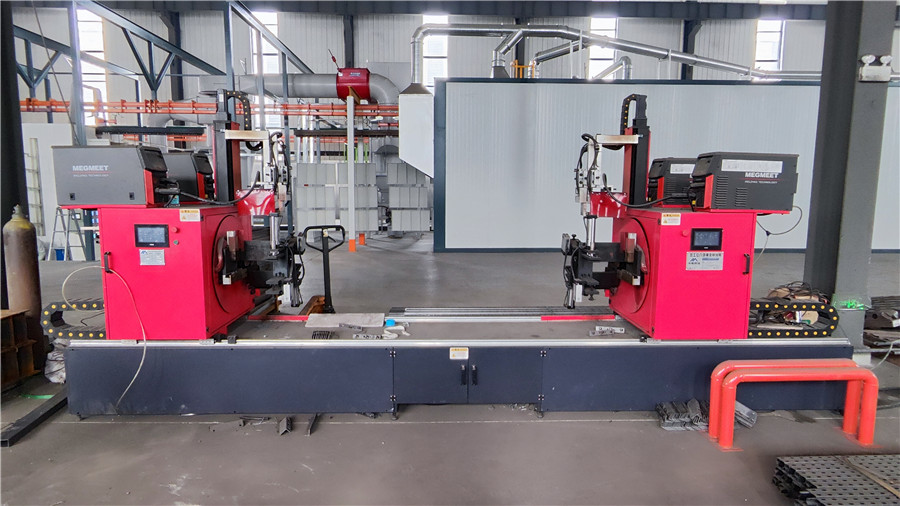
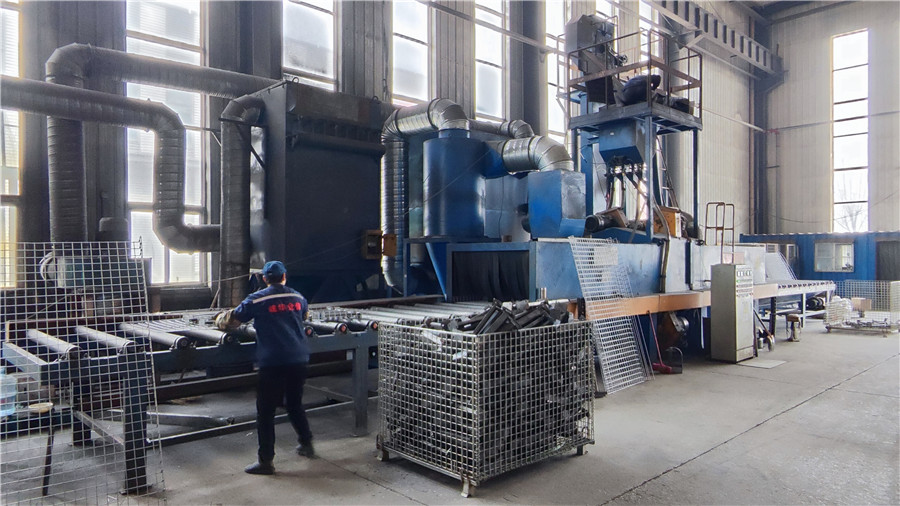
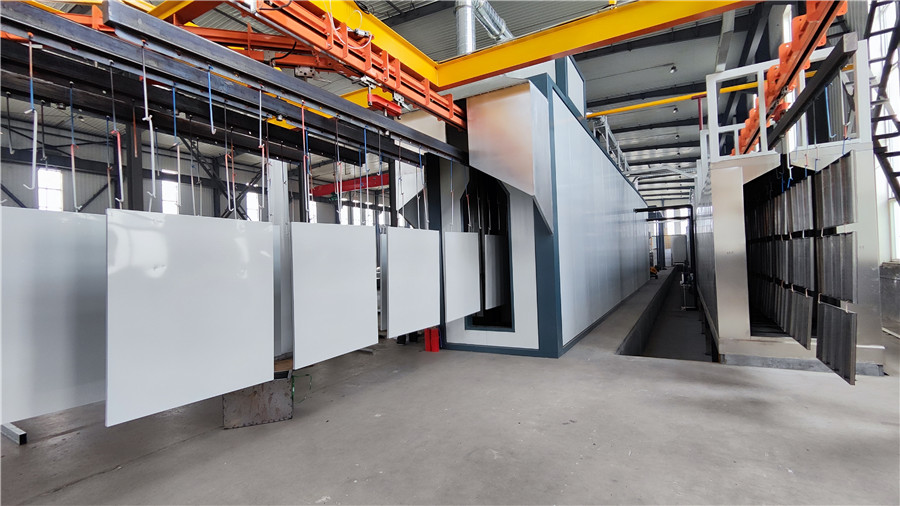
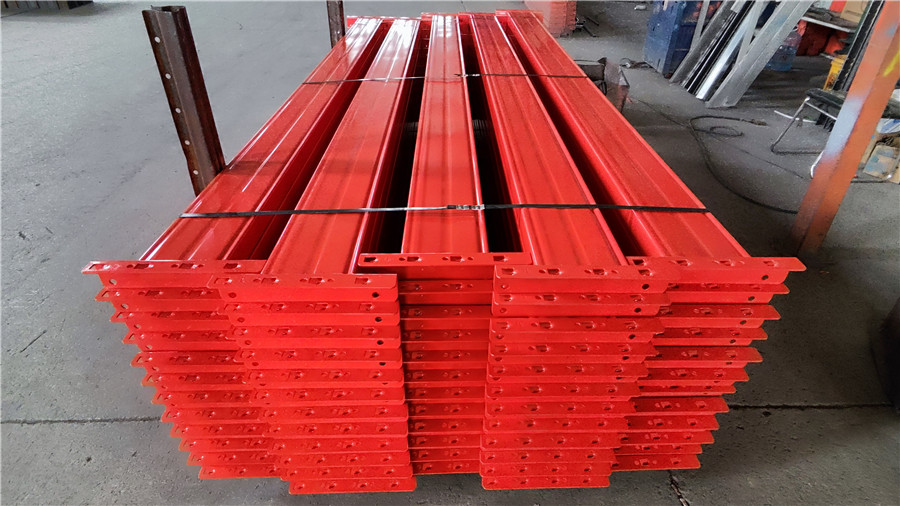
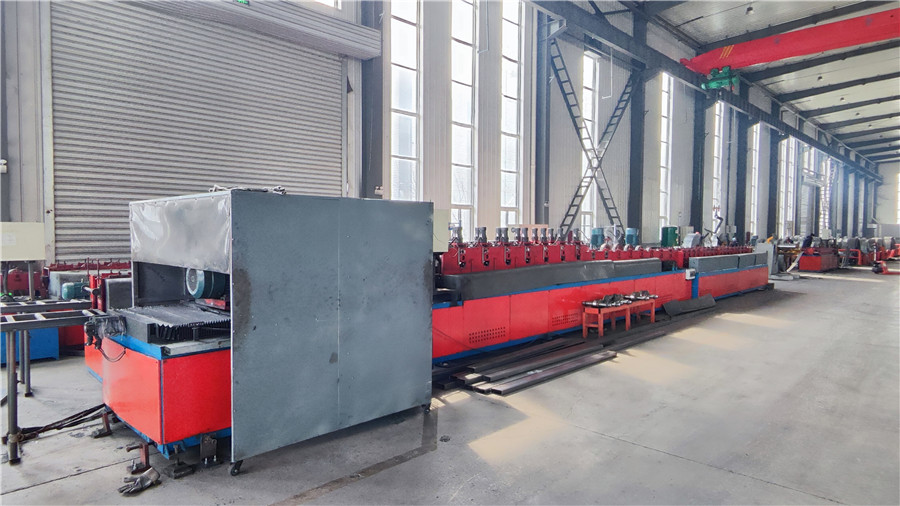
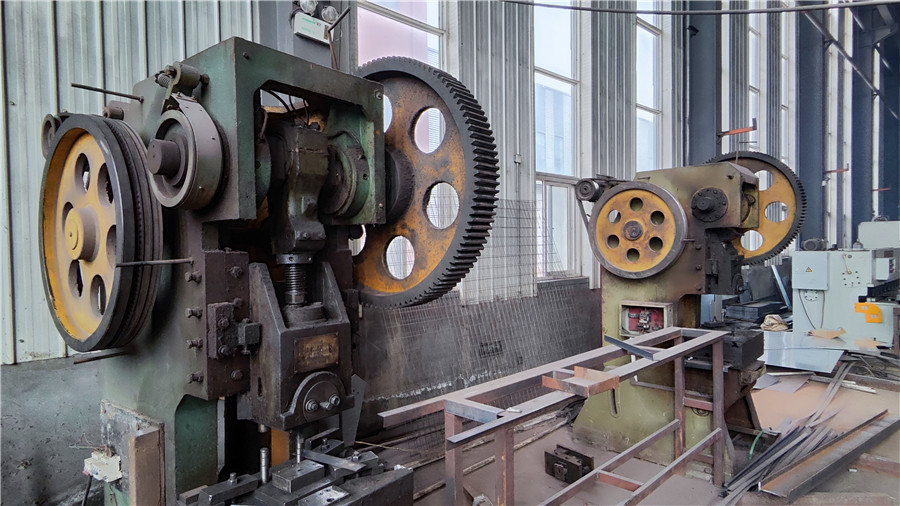
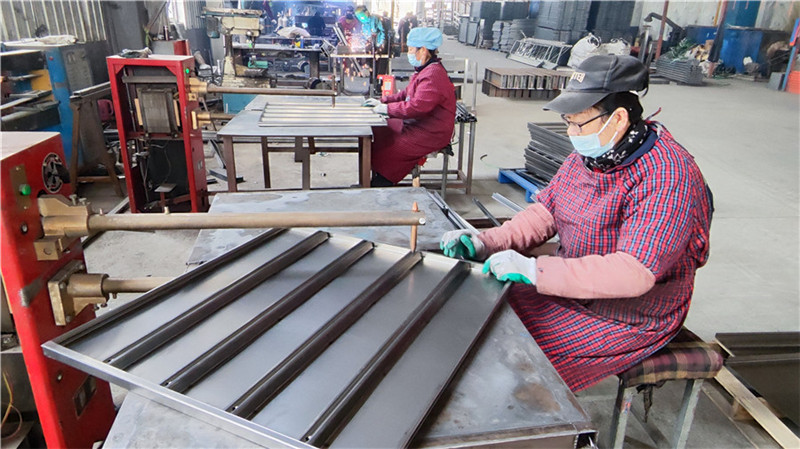
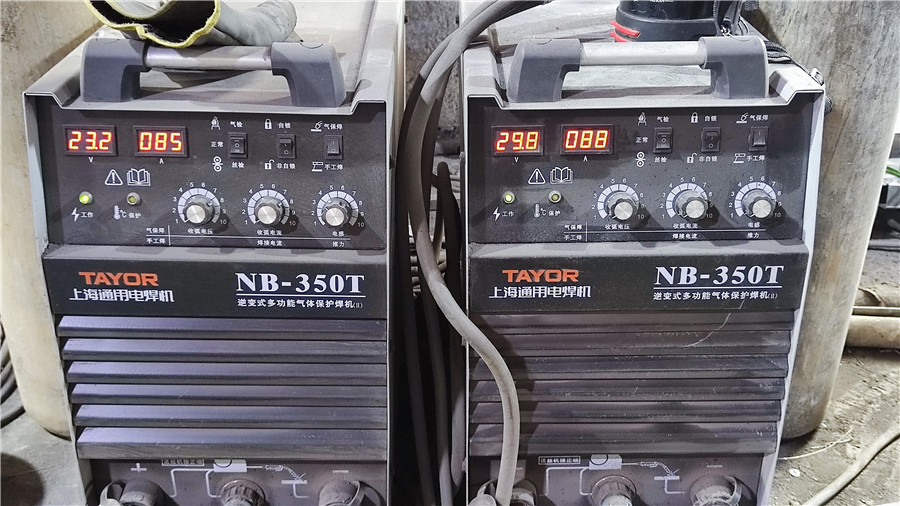
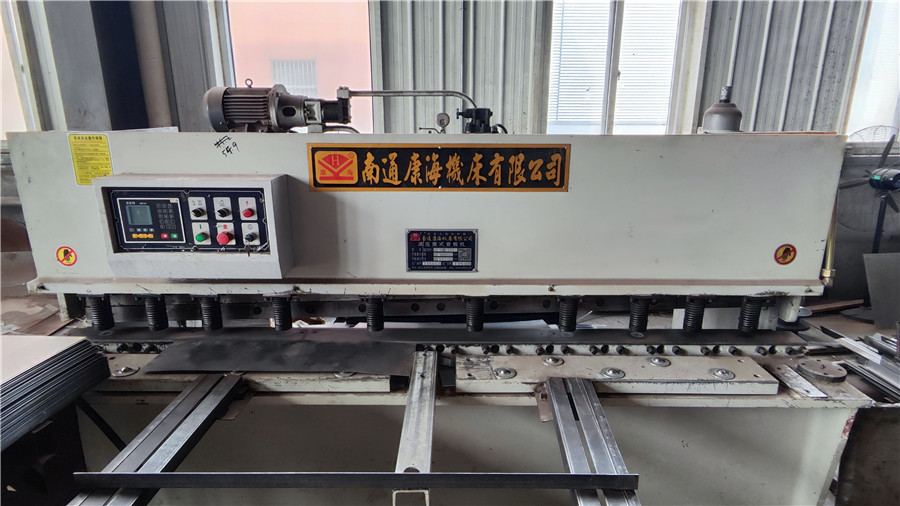
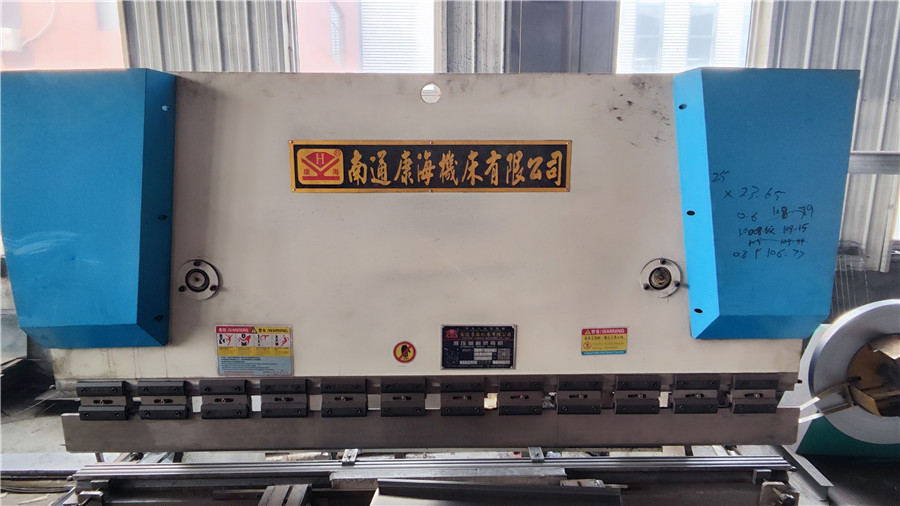
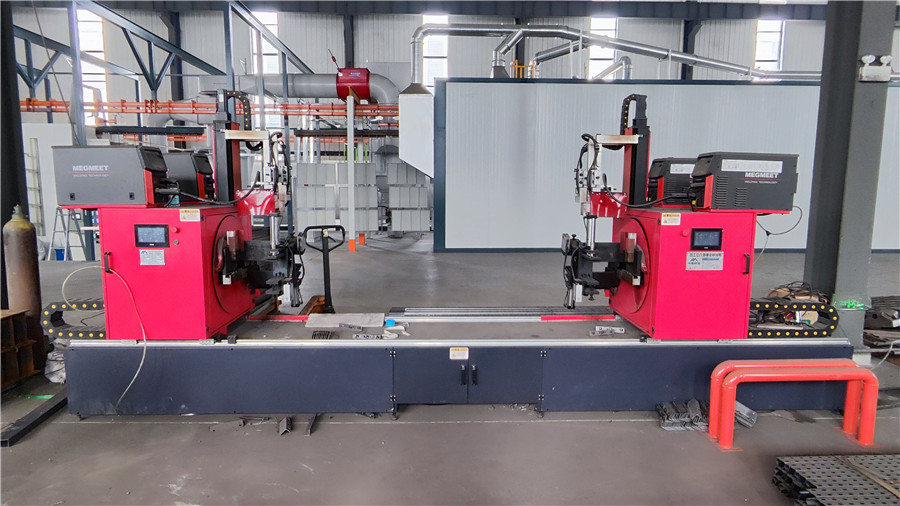
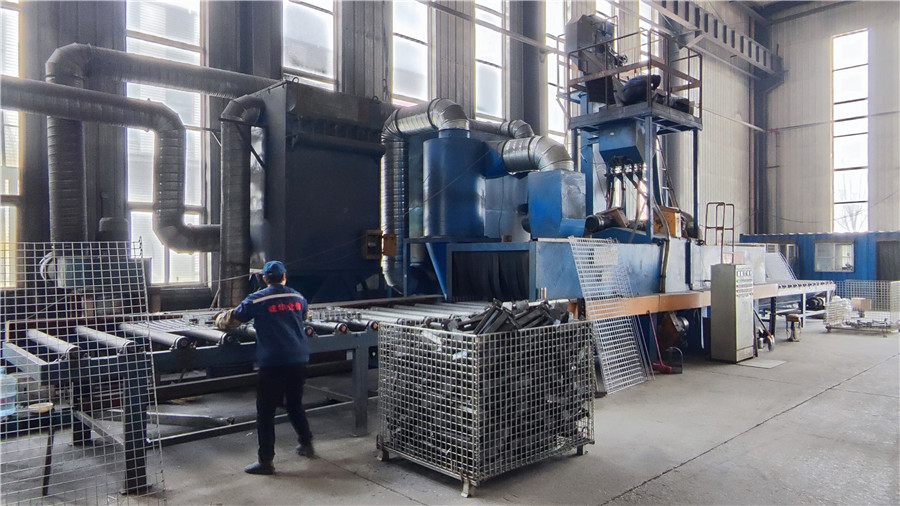
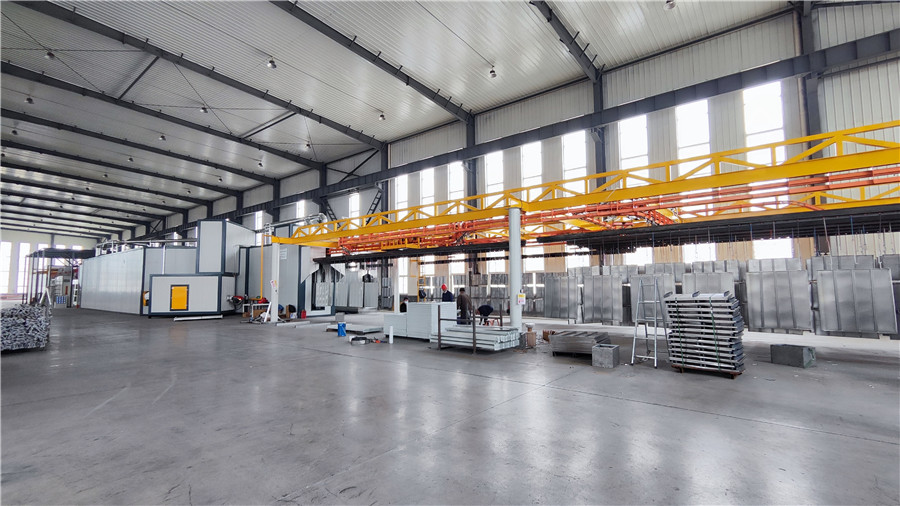
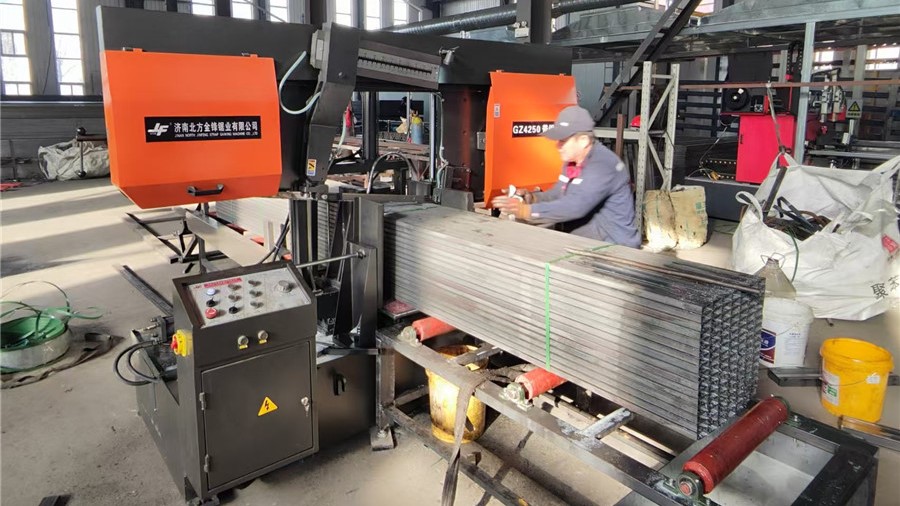
A transparent look inside our automated production lines, showcasing CNC bending, robotic mash welding, shot-blasting, and automated spray molding operations.
How top international exporters optimize CBM utilization, ensure zero-scratch transit, and streamline customs compliance across global sea routes.
By nesting back panels, utilizing interlocking upright bundling, and customizing carton dimensions for exact FEU/TEU ocean container profiles, manufacturers maximize CBM fill rates by up to 32%, drastically reducing per-unit shipping overhead for global distributors.
Export components undergo multi-layer packaging protocols: corner edge protectors, bubble cushioning wraps, high-density corrugated dividers, and heavy-duty shrink film wrapping. Metal surfaces stay moisture-free and rust-proof during trans-oceanic transit.
Comprehensive export documentation includes Mill Test Certificates (MTC), ISO 9001 quality compliance, Certificate of Origin (CO), and structural safety test reports complying with regional building safety codes across Europe, South America, and the Middle East.
Anticipating the technological convergence of smart IoT displays, automated guided vehicle (AGV) restocking interfaces, and carbon-neutral powder coating.
Next-generation gondola shelves incorporate continuous low-voltage busbars within upright columns, allowing seamless installation of Electronic Shelf Labels (ESL), smart shelf weight sensors, and digital strip displays without visible wiring clutter.
As automated shelf-replenishment robots become standard in hypermarkets, bottom shelf base legs are designed with reinforced structural clearance and laser-guided reflective indicators to support automated night-shift restocking.
Global environmental mandates require green manufacturing processes. Leading suppliers adopt low-temperature cure thermosetting powders and closed-loop water recycled shot-blasting, cutting carbon intensity per rack unit by over 25%.
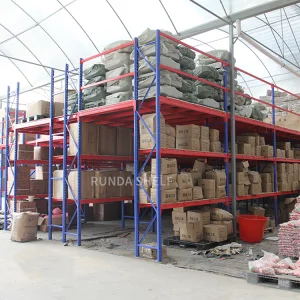
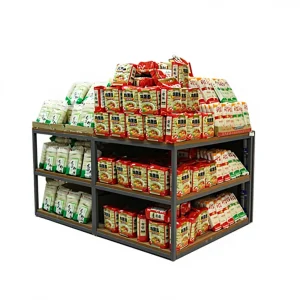
Double-sided island systems, mezzanine multi-tier racks, boutique snack shelving, and heavy-duty store storage solutions engineered for specialized retail verticals.
Addressing essential technical, quality control, engineering, and OEM/ODM sourcing queries for commercial retail leaders.
 DirectRack